Battery energy storage systems for manufacturing facilities can reduce billed peak demand, shift electricity purchases to lower-price periods and store surplus on-site solar generation. When the installation includes the required islanding and transfer equipment, storage can also support selected production loads during an outage. Its value depends on the plant load profile, tariff and electrical integration.
However, factory energy storage is not simply a matter of installing enough batteries to cover average electricity consumption. Production schedules, motor starting loads, continuous process requirements, power quality, and grid connection limits all influence the appropriate system design. This guide explains how industrial battery energy storage works in manufacturing environments, which applications offer measurable value, how to determine the required battery capacity, and what manufacturers should consider before selecting a system.
Manufacturing facilities often have more complex electrical demand patterns than offices or commercial buildings. Industrial machinery can consume substantial power during startup, acceleration, heating, cooling, or intensive production periods. For example, a factory may operate several production lines continuously while air compressors, injection molding machines, industrial chillers, and ventilation equipment cycle according to production requirements.
When multiple machines operate simultaneously, electricity demand can rise significantly above the normal operating level. Battery energy storage allows factories to manage these fluctuations without relying entirely on immediate electricity purchases from the grid.
| Manufacturing Challenge | Operational Impact | Potential Battery Storage Application |
|---|---|---|
| High Peak Electricity Demand | Demand charges increase when multiple machines operate simultaneously. | Battery discharge reduces grid demand during peak periods. |
| Time-of-Use Electricity Pricing | Production during expensive electricity periods increases operating costs. | Load shifting moves part of electricity purchasing into lower-cost hours. |
| Production-Related Power Interruptions | Equipment shutdowns can cause downtime, material losses, and restart expenses. | Engineered battery backup supports selected critical manufacturing loads. |
| Limited Grid Connection Capacity | Adding machinery may exceed the factory's contracted grid import capacity. | Battery storage can temporarily supplement available grid power. |
| Unused Solar Generation | Solar electricity generated during low-demand periods may be exported. | Battery storage shifts surplus solar energy into later production hours. |
| Frequent Production Load Changes | Power demand varies with machine operating cycles and production schedules. | An EMS coordinates charging and discharging with factory demand. |
The main advantage of an industrial battery energy storage system is the ability to separate the timing of electricity purchases from the timing of electricity consumption. For example, suppose a manufacturing plant normally operates at 1,200 kW but reaches 1,600 kW during periods of simultaneous equipment operation.
If the factory aims to keep grid demand below 1,300 kW, the battery must supply up to:
1,600 kW − 1,300 kW = 300 kW
If the required 300 kW reduction is constant for two hours, the required AC energy output is approximately:
300 kW × 2 hours = 600 kWh
The battery's installed nominal capacity must be higher after considering usable state-of-charge limits, conversion losses, and battery aging. This calculation illustrates why industrial battery storage design should begin with the actual production load profile.
A factory battery energy storage system stores electricity in rechargeable battery cells and releases it when required by the facility. In a typical behind-the-meter installation, the battery system connects to the factory's electrical distribution network through power conversion and protection equipment. During low-demand or lower-price periods, electricity charges the battery. When manufacturing electricity demand increases, the battery discharges to supplement power from the grid.
The energy management system coordinates this process according to production demand, electricity tariffs, battery operating limits, and available renewable generation.
| Component | Main Function | Importance for Manufacturing |
|---|---|---|
| Battery Cells and Modules | Store electrical energy. | Determine battery capacity, chemistry, and cycling characteristics. |
| Battery Management System (BMS) | Monitors voltage, current, temperature, and state of charge. | Maintains battery operation within defined electrical and thermal limits. |
| Power Conversion System (PCS) | Converts electricity between AC and DC. | Controls the battery's charging and discharging power. |
| Energy Management System (EMS) | Schedules battery charging and discharging. | Coordinates battery operation with electricity tariffs and production schedules. |
| Thermal Management System | Controls battery operating temperature. | Supports battery performance under changing industrial operating conditions. |
| Electrical Protection Equipment | Provides fault detection, electrical isolation, and protection coordination. | Supports integration with the factory's existing electrical distribution system. |
| Fire Detection and Protection Systems | Provides detection, emergency response, and protective functions. | Supports industrial installation safety requirements. |
Industrial energy storage buyers must distinguish between battery power and energy capacity. Power capacity (kW or MW) determines how much electricity the system can deliver at one time. Energy capacity (kWh or MWh) determines how much electricity the battery can store.
For example:
A 500 kW / 1,000 kWh system has a nominal energy-to-power ratio of two hours.
A 500 kW / 2,000 kWh system has a nominal energy-to-power ratio of four hours.
A 1,000 kW / 2,000 kWh system has a nominal energy-to-power ratio of two hours.
Actual discharge duration depends on usable battery capacity, state-of-charge limits, discharge efficiency, auxiliary energy consumption, temperature, and degradation. A four-hour nominal ratio does not automatically guarantee four hours of full AC output under all operating conditions.
Peak shaving is one of the most direct applications of battery storage in manufacturing facilities. Many industrial electricity tariffs include a demand charge based on the highest measured electricity demand during a billing period. Even a relatively short production peak can affect the factory's monthly electricity expenses.
Consider a manufacturing plant with the following electricity demand:
Normal operating demand: 1,200 kW
Maximum demand during production peaks: 1,600 kW
Target maximum grid demand: 1,300 kW
Assumed industrial demand charge: $18/kW/month
The battery must reduce grid demand by:
1,600 − 1,300 = 300 kW
Monthly gross demand-charge savings:
300 kW × $18/kW = $5,400
If this reduction is achieved in all 12 billing months:
Annual gross demand-charge savings = $64,800
This is an illustrative calculation, not a measured project result. Actual savings depend on the utility's demand-charge rules, the duration and timing of factory demand peaks, and battery availability. Some industrial tariffs also include ratchet charges or separate demand measurements for different time periods. These rules should be included in the dispatch model.
Factories operating two or three shifts may consume substantial electricity during expensive tariff periods. Battery storage can reduce costs by charging when electricity is cheaper and discharging during higher-price periods.
Suppose a manufacturing facility operates under the following tariff:
Off-peak electricity price: $0.08/kWh
Peak electricity price: $0.22/kWh
Battery AC-to-AC round-trip efficiency: 85%
Daily battery electricity delivered: 1,000 kWh
Any efficiency used in an initial financial example is a modeling assumption. For equipment selection, use the proposed system efficiency at the agreed measurement boundary, including the treatment of PCS losses and auxiliary consumption.
To deliver 1,000 kWh, the system must purchase approximately:
1,000 ÷ 0.85 = 1,176.5 kWh
Charging electricity cost:
1,176.5 × $0.08 = $94.12
Avoided peak electricity purchase:
1,000 × $0.22 = $220
Gross daily energy arbitrage benefit = $125.88
For 300 operating days:
Annual gross benefit = approximately $37,765
This figure excludes battery degradation, maintenance, financing, and other operating expenses. The key consideration is whether the factory has enough low-price charging time and sufficient battery capacity to discharge during expensive production hours.
Factories frequently have large roofs suitable for photovoltaic installations. However, solar electricity generation may not match the timing of production demand. A factory operating evening or night shifts may have substantial electricity demand after solar generation has declined. Similarly, a factory that reduces production during weekends may generate more solar electricity than it can consume immediately. Battery storage helps shift this electricity to later production periods.
For example, suppose a factory generates 2,000 kWh of surplus solar electricity during a low-demand day.
At an assumed 85% AC-to-AC round-trip efficiency, the battery could deliver approximately:
2,000 kWh × 85% = 1,700 kWh
If the electricity purchase price during the later production period is $0.20/kWh, the gross avoided purchase value would be:
1,700 × $0.20 = $340
However, the incremental benefit must subtract the compensation that the factory would otherwise receive for exporting the electricity, along with battery-related costs.
For instance, if the alternative export payment were $0.05/kWh, the incremental daily value would be:
$340 − (2,000 × $0.05) = $240
This calculation assumes all surplus electricity can be stored and subsequently used. Actual benefits depend on the site's generation profile, battery availability, export regulations, and tariff structure.
Power interruptions can have consequences beyond the immediate loss of electricity. Depending on the manufacturing process, an unexpected shutdown may result in rejected materials, unfinished products, equipment resets, process stabilization time, and delayed shipments. Battery storage can support selected critical loads if the installation is engineered for backup operation.
Potential critical loads include:
Industrial control systems and PLC equipment
Production monitoring and communication networks
Selected process pumps and cooling equipment
Critical instrumentation
Designated automation equipment
Essential facility safety and control systems
Consider a production facility with 150 kW of selected critical loads that must remain powered for two hours.
Required usable AC energy:
150 kW × 2 hours = 300 kWh
Assuming an 85% usable energy fraction and 94% discharge-path efficiency:
Required nominal battery capacity:
300 ÷ (0.85 × 0.94) = approximately 375 kWh
Additional reserves and end-of-life capacity allowances may increase this requirement. A standard grid-connected energy storage system does not automatically function as an uninterruptible power supply. Continuous or near-instantaneous backup requires suitable transfer equipment, islanding controls, inverter capability, and protection coordination. Sensitive manufacturing equipment may still require a dedicated UPS.
Manufacturers expanding production may need additional electricity capacity to operate new equipment. However, increasing grid connection capacity can involve transformer replacement, utility infrastructure upgrades, or lengthy approval processes. Battery storage may provide an alternative for short-duration demand increases.
For example:
Factory grid import limit: 2,000 kW
Existing production load: 1,700 kW
Additional production equipment demand: 500 kW
Total requested demand: 2,200 kW
A battery supplying 200 kW could keep grid import at the 2,000 kW limit while sufficient stored energy remains available.
If this demand occurs for 90 minutes:
200 kW × 1.5 hours = 300 kWh
However, battery storage cannot indefinitely replace grid infrastructure when the additional demand continues for long periods. The factory must also have sufficient time and available grid capacity to recharge the battery between high-demand events.
Different manufacturing processes create different opportunities for industrial energy storage. The suitability of a battery system depends on the production schedule, machinery characteristics, tariff structure, and required operating duration.
| Manufacturing Industry | Typical Electrical Loads | Potential Energy Storage Benefits |
|---|---|---|
| Automotive Manufacturing | Robotic assembly lines, welding equipment, compressors, and production machinery. | Peak demand management, electricity cost optimization, and selected control-system backup. |
| Metal Fabrication | CNC machines, welding systems, electric furnaces, and industrial motors. | Management of short demand peaks and selected load shifting. |
| Food and Beverage Processing | Refrigeration, packaging lines, pumps, and processing equipment. | Peak shaving, solar integration, and backup for designated refrigeration controls. |
| Textile Manufacturing | Spinning machines, weaving equipment, drying systems, and HVAC. | Time-of-use load shifting and electricity demand management. |
| Electronics Manufacturing | Automated production equipment, HVAC, cleanroom systems, and process controls. | Energy cost optimization and engineered support for selected critical electrical loads. |
| Plastics Manufacturing | Injection molding machines, extrusion lines, chillers, and compressors. | Peak demand reduction and improved utilization of on-site solar generation. |
For facilities with highly variable electrical loads, detailed interval data is particularly important. Some machines create short starting-current transients that require separate power-quality solutions or appropriate inverter capabilities. Battery energy capacity alone does not establish whether the system can support those events.
Begin with at least a year of interval electricity data and identify the production processes behind the largest peaks. Separate the demand that can be shifted by scheduling from the demand that requires battery discharge. Include compressors, chillers, furnaces, welding equipment and other large loads where relevant to the plant. For each candidate system, check continuous AC power, usable energy at the required future capacity, motor-starting requirements and the available recharge window. Daily consumption is useful context, but the energy above the target import limit determines a peak-shaving requirement.
Model backup separately from routine energy management. Define the critical circuits, the acceptable interruption time and the minimum state of charge that must be reserved. A battery cabinet alone does not establish those functions. Before procurement, agree the connection point, outage work needed for installation and the interfaces between the battery, PCS, EMS and existing protection. This makes the proposal relevant to the actual plant instead of relying on a generic capacity range.
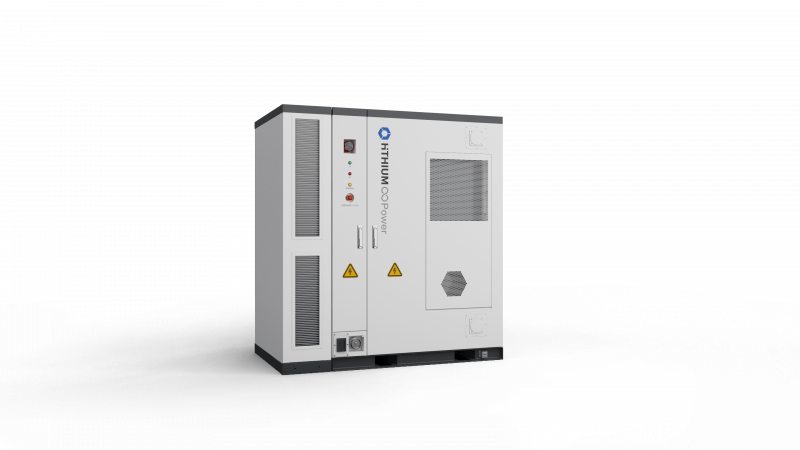
The project references in HiTHIUM's C&I products and solutions catalogue include a containerized 8.36 MW/16.72 MWh installation in Hamburg, Germany, using SMA PCS for peak-valley electricity arbitrage. A 9 MW/18.79 MWh project in Romania is integrated with the customer's photovoltaic system to store surplus generation and support electricity arbitrage. The catalogue also describes a 1.75 MW/3.65 MWh cabinet installation in Baktalórántháza, Hungary, for industrial energy management. These references illustrate different project scales and integration arrangements. They do not establish a common payback period or annual saving for all manufacturing facilities.
For a plant evaluating similar applications, compare the reference project with its own voltage, operating schedule, peak duration and PCS requirements. Ask for project-specific operating evidence when assessing production continuity or investment returns.
Industrial battery storage projects require equipment that can meet the factory's power demand, discharge duration, environmental conditions, and expansion requirements. HiTHIUM develops lithium iron phosphate (LFP) battery technology and energy storage products for commercial and industrial applications. Its commercial and industrial energy storage solutions can be evaluated for manufacturing applications such as peak-valley electricity management, on-site solar integration, and industrial power demand optimization.
| HiTHIUM product | Nominal battery energy | Power conversion arrangement | Relevant application |
|---|---|---|---|
| ∞Block 125kW/261kWh | 261 kWh | Integrated AC/DC all-in-one configuration with 125 kW nominal AC power | Modular demand management and solar storage |
| ∞Block 418kWh | 418 kWh class | DC battery cabinet with a separately matched PCS | Projects using a coordinated battery and PCS solution |
| ∞Power 1022kWh | 1022.72 kWh | Battery cabinet matched with an external PCS; the catalogue describes a 250 kW solution | Approximately 1 MWh per battery cabinet for multi-hour storage |
HiTHIUM can work with PCS manufacturers to provide a coordinated battery and power conversion solution. The final quotation should identify the battery, PCS model, EMS, switchgear, transformer where required, and commissioning scope. Nominal battery energy is not the same as usable AC energy, and the catalogue configuration must be matched to the local grid and operating requirements.
These products use LFP batteries with liquid cooling to manage cell temperatures during operation. Cooling capability and any power derating must be checked against the plant ambient conditions and duty cycle. The ∞Power 1022kWh battery cabinet occupies approximately 3.4 m². This is the battery cabinet footprint only. The complete installation also needs space for the external PCS, service access, safety clearances and any other site equipment. Explore the HiTHIUM C&I battery storage product range and commercial and industrial energy storage solutions when comparing configurations.
Industrial battery storage must be integrated with the factory's existing electrical infrastructure without compromising equipment protection or personnel safety. Unlike standalone electrical equipment, an energy storage system may both consume and supply power. This bidirectional operation requires appropriate protection coordination and control logic.
Battery storage safety depends on cell chemistry, thermal management, electrical protection, fire detection, system controls, and installation conditions. Lithium iron phosphate batteries are widely used in stationary storage applications because of their thermal characteristics and suitability for repeated charging and discharging.
However, LFP systems are not free from thermal runaway or fire risks.
Depending on project location and system architecture, relevant standards and codes may include:
IEC 62619: Safety requirements for secondary lithium cells and batteries used in industrial applications.
IEC 62933 Series: Requirements addressing electrical energy storage systems.
UL 9540: Safety standard for energy storage systems and equipment.
UL 9540A: Test method evaluating thermal runaway fire propagation characteristics.
NFPA 855: Standard for installation of stationary energy storage systems.
These references do not establish that every product holds every listed certification. Manufacturers should request documentation applying to the exact supplied model and configuration.
Industrial electrical networks may contain equipment that produces harmonics, rapid load changes, and substantial starting currents.
Before installation, engineers should evaluate:
Voltage compatibility
Transformer and switchgear ratings
Short-circuit protection
Harmonic distortion
Power factor requirements
Grounding and electrical isolation
PCS response characteristics
Coordination with existing UPS and generator equipment
Industrial battery storage should not be assumed to solve all power quality problems automatically. For applications involving voltage disturbances, motor-starting events, or sensitive automation equipment, the required inverter capabilities and protection arrangements must be explicitly specified.
Manufacturing electricity demand is strongly influenced by production planning. For example, a factory may have predictable periods when production lines start, large motors operate simultaneously, or industrial cooling systems reach their maximum demand. Integrating production schedules into the battery EMS can help reserve stored energy for these periods. This strategy can also reduce unnecessary battery cycling during periods when production demand is already low.
Fixed charging and discharging schedules may not respond adequately to changing production volumes, electricity tariffs, or solar generation. Advanced energy management systems can use load forecasts, tariff information, weather conditions, and battery state of charge to determine operating schedules. One approach is model predictive control (MPC), which repeatedly updates charging and discharging decisions as new information becomes available. For factories with variable production demand, forecast-based operation can improve the coordination of peak shaving, energy arbitrage, and reserve capacity.
Any performance improvement should be verified against a consistent operating baseline rather than assumed from the control technology alone.
Battery usable capacity gradually changes with cycling and calendar aging.
Important factors include:
Depth of discharge
Operating temperature
Charging and discharging rates
Time spent at high state of charge
Annual energy throughput
Manufacturers should evaluate whether the selected system can continue meeting required power and energy targets near the end of its intended operating life.
Future production expansion should also be considered.
New machinery, additional production shifts, process electrification, and increased cooling demand may change the factory's electricity requirements. Modular energy storage systems can provide expansion opportunities, but compatibility between existing and future equipment should be verified before procurement.
After installation, factory operators should compare actual electricity savings against the original project model.
Useful performance indicators include:
Monthly grid demand reduction in kW
Electricity shifted between tariff periods in kWh
Battery charging and discharging energy
Measured round-trip efficiency
Annual electricity cost savings
Battery availability
Capacity retention and degradation trends
Maintenance and auxiliary energy consumption
Production volume, weather, electricity tariffs, and operating schedules should be considered when comparing performance across different periods. This helps distinguish battery-related benefits from changes caused by unrelated factory operations.
The required size depends on maximum grid demand, the intended power reduction, discharge duration, and the factory's operating schedule. For example, supplying 500 kW for two hours requires 1,000 kWh of usable AC energy. Installed battery capacity must also account for conversion losses, usable state-of-charge limits, operating reserves, and degradation. A detailed analysis of at least 12 months of electricity demand data is recommended.
Yes. Battery storage can reduce manufacturing electricity expenses through peak shaving, time-of-use load shifting, and improved solar self-consumption. The financial benefit depends on the factory's demand charges, electricity price differences, operating patterns, and battery efficiency. Actual savings should be calculated using the facility's tariff and measured load profile.
A properly engineered battery backup system can support selected manufacturing loads during an outage. However, continuous production depends on the required power, available energy capacity, inverter capability, transfer arrangements, and compatibility with the factory's equipment. Sensitive machinery may require a dedicated UPS, while long-duration production backup may require additional generation or energy storage capacity.
Battery lifetime depends on chemistry, operating temperature, depth of discharge, cycling frequency, and maintenance. Buyers should review the manufacturer's specified cycle-life conditions, calendar-life assumptions, guaranteed capacity retention, energy throughput, and warranty limitations. Project financial models should account for degradation throughout the intended operating period.
Many operating factories can be evaluated for battery storage retrofits. Installation feasibility depends on available space, electrical distribution capacity, transformer and switchgear compatibility, environmental conditions, safety requirements, and utility interconnection rules. A factory electrical assessment should determine the appropriate connection arrangement and whether equipment upgrades are necessary.
Battery energy storage systems for manufacturing facilities can help factories manage peak electricity demand, reduce energy purchases during expensive tariff periods, increase solar self-consumption, and support selected critical electrical loads. The most effective industrial energy storage projects begin with measurable production and electricity requirements. Power capacity, usable energy, discharge duration, round-trip efficiency, system safety, and lifecycle cost should determine the final design.
For manufacturers operating multiple shifts, expanding production capacity, or integrating on-site renewable generation, HiTHIUM provides commercial and industrial battery energy storage solutions based on LFP battery technology, liquid-cooled cabinets, and modular energy storage configurations. Its portfolio includes ∞Block 261kWh and 418kWh cabinets and the higher-capacity ∞Power 1022kWh system, providing options for different industrial energy storage requirements.
Before requesting a system proposal, prepare your factory's electricity tariff, 12-month load profile, production schedule, installation conditions, existing solar generation capacity, and expected energy storage objectives. Contact HiTHIUM to discuss your manufacturing facility's energy requirements, product specifications, and suitable industrial battery energy storage configurations.

 Previous: